Definition and Scope of Manual CNC Machines
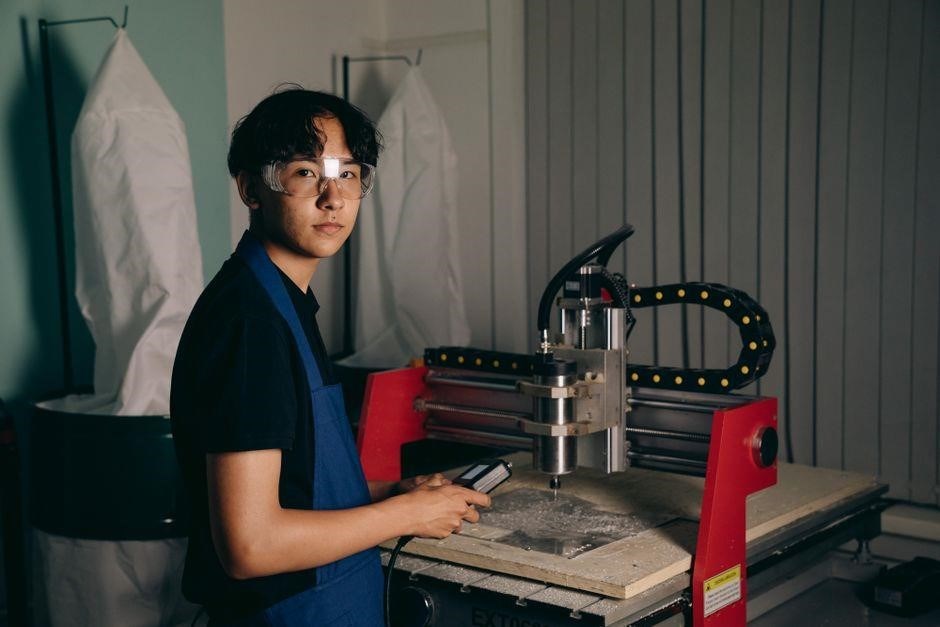
Manual CNC machines blend hand‑operated controls with computer‑guided motion‚ enabling precise machining without full automation․ They allow operators to input G‑code‚ adjust parameters on‑the‑fly‚ and perform tasks such as milling‚ drilling‚ or routing with direct human oversight․ for hobbyists!
Manual CNC Machines: Overview of Hardware‚ Control‚ and Applications
Manual CNC systems marry traditional mechanical components with computer‑controlled motion‚ offering a flexible platform for small‑scale production and prototyping․ The core hardware typically includes a spindle motor‚ linear drives‚ guide rails‚ and a tool‑holding fixture that can be swapped manually․ Operators load G‑code files directly onto the machine’s control board‚ often via a USB stick or a basic terminal interface‚ and then fine‑tune cutting parameters—feed rate‚ spindle speed‚ and depth of cut—through a handheld keypad or a basic LCD display․ This hybrid approach preserves the tactile feedback of manual operation while harnessing the precision of CNC motion control․ Applications span woodworking‚ metalworking‚ and hobbyist projects; from engraving custom wooden signs to milling small aluminum brackets‚ the system’s versatility makes it ideal for makers who need repeatable accuracy without the cost of a fully automated cell‚ empowering creators to produce complex geometries with minimal setup time․ The platform’s low‑cost design makes it ideal for educational labs‚ enabling students to practice tool‑path programming and machining․ Integrated sensors record spindle torque and vibration‚ providing real‑time diagnostics for process improvement․ Community firmware updates often add safety features like automatic spindle shutdown on over‑current detection‚ enhancing operator confidence expanding possibilities․
Core Mechanical Components of Manual CNC Systems
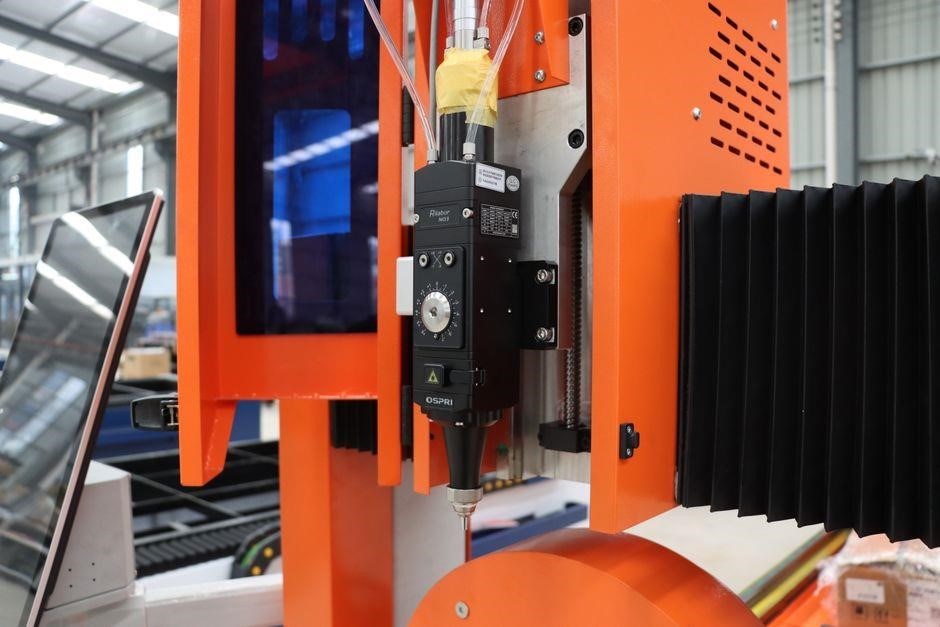
Manual CNC machines combine a spindle motor‚ linear drives‚guide rails‚and a tool holder․ Operators input G‑code and adjust feed‚ speed‚ and depth manually․ This setup suits hobbyistsand production‚ delivering cuts without full automation․
Spindle Motors‚ Linear Drives‚ Guide Rails‚ and Tool Housing
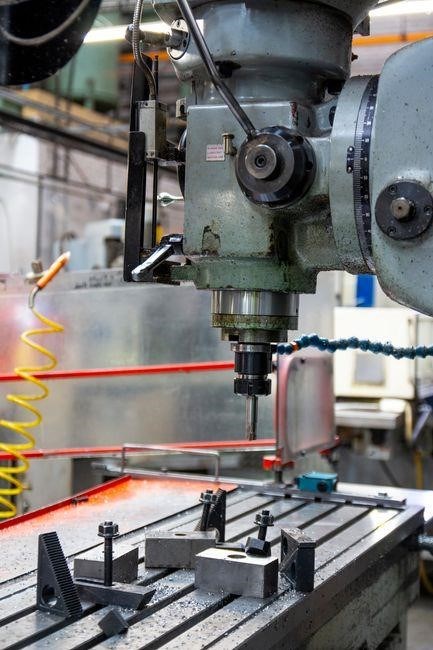
Manual CNC machines rely on a combination of spindle motors‚ linear drives‚ guide rails‚ and tool housings to deliver accurate machining while still allowing operator control․ The spindle motor‚ typically a 3 phase induction or DC unit‚ provides the rotational power needed for cutting tools․ Its RPM range can be manually adjusted via a hand wheel or a simple potentiometer‚ giving the operator instant feedback on speed changes without a full computer interface․ Linear drives‚ often bearing or driven‚ translate the motor’s rotation into linear motion along the X‚ Y‚ and Z axes․ In many hobbyist setups‚ these drives are driven by stepper motors that can be manually stepped or commanded through a basic joystick‚ allowing the operator to fine tune feed rates and positioning․ Guide rails‚ usually made from hardened steel or aluminum‚ serve as the backbone of the machine’s accuracy․ They support the carriage and ensure that motion remains straight and repeatable․ The rails are often paired with precision linear bearings that reduce play and vibration‚ which is crucial when the machine is not fully automated․ Tool housings‚ or collets‚ clamp the cutting tool securely and can be swapped quickly by the user․ In manual systems‚ the housing is typically a simple type or design that lets the user change tools without specialized tooling․ Together‚ these components create a system that balances the tactile feel of operation with the precision of guided motion‚ making manual CNC machines ideal for prototyping‚ production and educational environments where full automation is unnecessary or prohibitive․ Operators often calibrate the system before each job‚ checking spindle speed‚ axis alignment‚ and tool offsets to maintain consistency․ This ensures each part meets tolerances and reduces scrap․
Control Systems and Human-Interface Operations
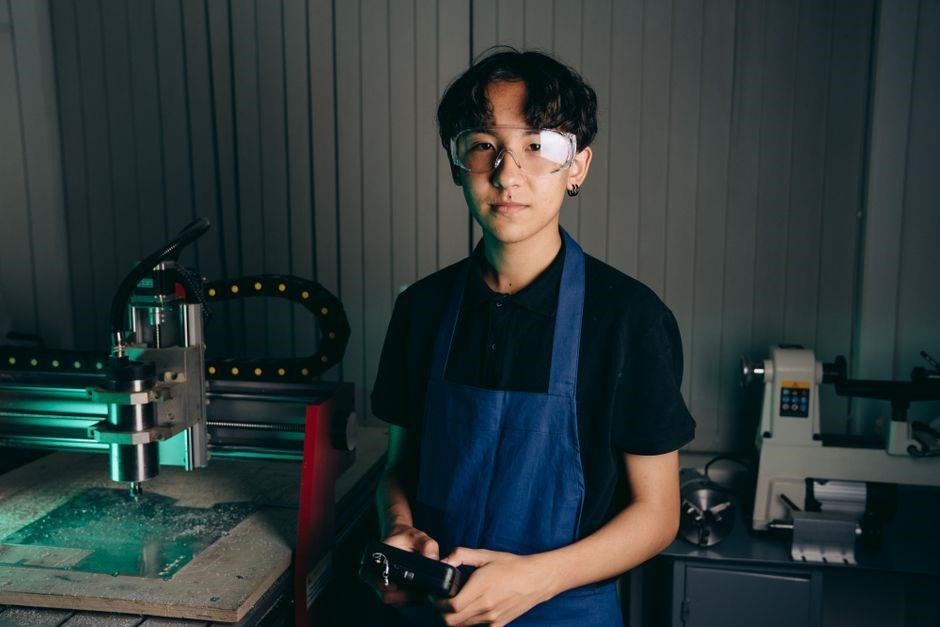
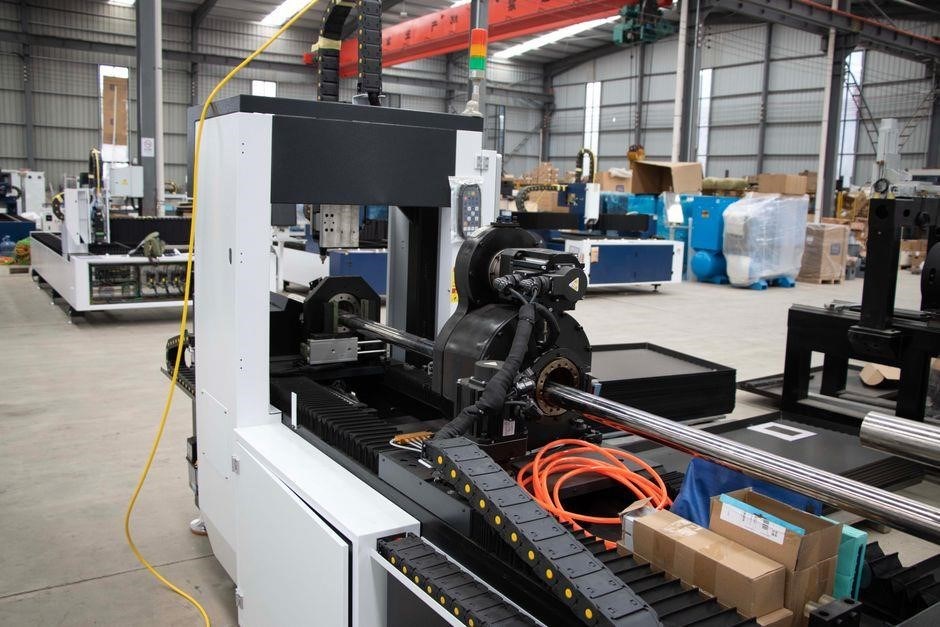
Manual CNC control relies on simple interfaces: a hand‑wheel or joystick for axis movement‚ a dial for spindle speed‚ and a basic LCD for status․ Operators enter G‑code via a small keyboard or USB‚ then adjust feed rates in real time‚ watching the machine’s live feed on the display․ for fine
Manual G-code Entry‚ Software Editing‚ and Real-time Parameter Adjustment
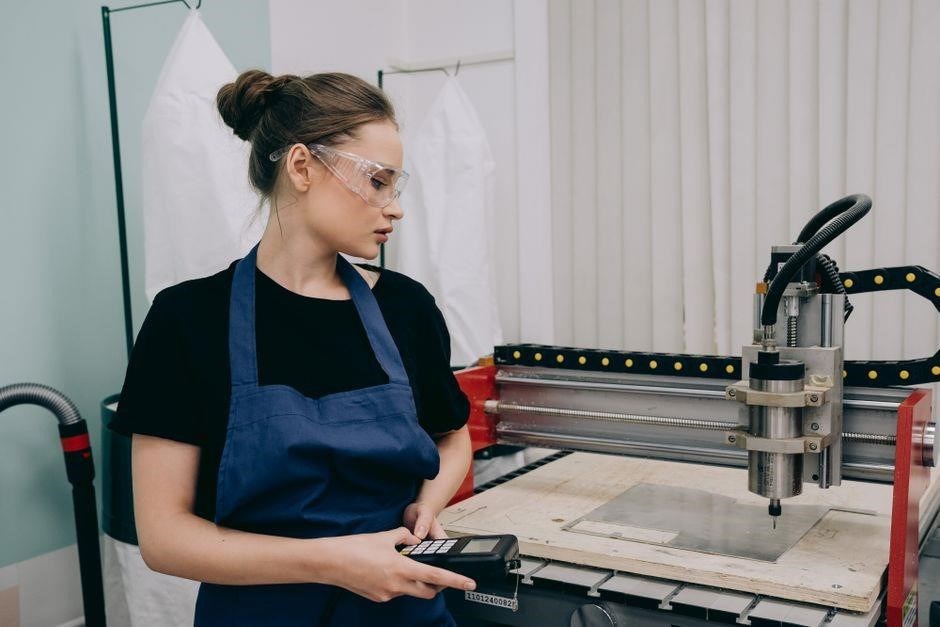
Manual CNC systems empower operators to craft G‑code directly on the machine using a compact keypad‚ rotary encoder‚ or touch interface․ Each line is entered sequentially‚ and the firmware immediately validates the syntax‚ displaying the parsed command on a small LCD․ This instant feedback loop allows the user to catch errors before the spindle starts‚ reducing waste and improving safety․
For more elaborate parts‚ a lightweight editor on a laptop or tablet can be employed․ The programmer writes the full program in a plain‑text editor‚ then saves it in a standard ․nc or ․gcode format․ The file is transferred via USB‚ SD card‚ or serial port to the CNC controller․ Once loaded‚ the operator can review the program line by line‚ using the machine’s display to step through the code and verify tool paths visually․
During operation‚ the operator retains full control over critical parameters․ The control panel offers knobs or sliders to adjust feed rate‚ spindle speed‚ and retract distance on the fly․ By pausing the cycle‚ the user can tweak these values‚ observe the effect on the workpiece‚ and resume without restarting the entire program․ This real‑time adjustment is vital for compensating material inconsistencies‚ correcting tool wear‚ or fine‑tuning the finish․
Many manual systems also support live coordinate monitoring and automatic zeroing․ The operator can set the workpiece origin at any point‚ then use the machine’s jog functions to position the tool precisely․ Error messages‚ such as limit‑switch triggers or spindle overload warnings‚ are displayed immediately‚ allowing rapid response․ By blending manual code entry‚ external editing‚ and dynamic parameter control‚ users achieve the precision of CNC machining while preserving the flexibility and immediacy of hands‑on operation․
Operational Workflow and Machining Strategies
Operators begin by mounting the workpiece‚ then manually zero the tool․ They load G‑code‚ set feed and spindle speeds‚ and run a dry test․ Once verified‚ the machine cuts with hand‑guided adjustments for depth and tool changeovers‚ ensuring precision and safety․ Monitor spindle‚ adjust feed․
Feed Rates‚ Depth of Cut‚ Tool Changeovers‚ and Workpiece Setup
Manual CNC operation begins with a precise workpiece setup: secure the material on the table‚ apply a reliable clamping system‚ and verify spindle zeroing․ Once the fixture is locked‚ the operator inputs the feed rate‚ typically expressed in inches per minute (IPM) or millimeters per second (mm/s)․ For materials very‚ like thin wood or soft aluminum‚ lower feed rates reduce chatter and preserve tool life․ Heavier cuts use higher rates while maintaining a safe depth of cut‚ usually 0․01–0․05 inches per pass for milling and 0․02–0․1 inches for drilling․ Depth of cut is adjusted incrementally; a pass that removes too much material can overload the spindle or cause deflection․ A common strategy is to perform a roughing pass to remove bulk material‚ followed by a finishing pass that reduces the depth to 0․001–0․003 inches for a smooth surface․ Tool changeovers are handled manually: the operator lifts the spindle‚ swaps the bit‚ and re‑zeroes the tool․ During this step‚ the machine’s tool‑change routine is triggered by a button press‚ and the operator verifies the new tool length with a dial indicator․ The entire workflow is monitored in real time; the operator watches the spindle speed‚ feed rate‚ and torque readouts on the control panel‚ adjusting parameters on the fly if vibration or overheating is detected․ By combining setup‚ feed and depth selection‚ and tool changes‚ a manual CNC machine delivers precise‚ repeatable results even without full automation․
Safety‚ Shielding‚ and Risk Management Practices
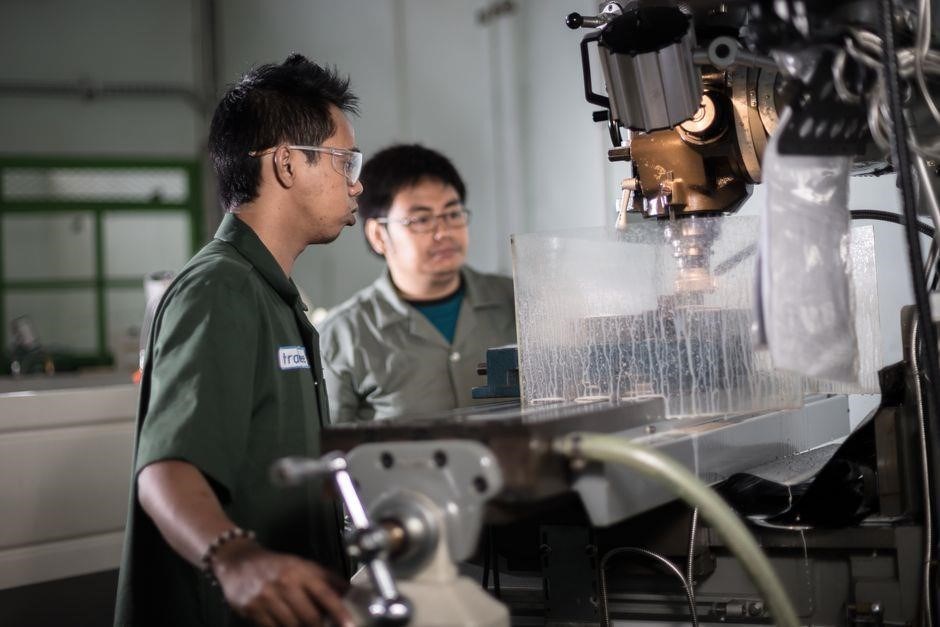
Operators must wear eye protection‚ gloves‚ and hearing guards․ Enclosures with interlocks stop the spindle when opened․ Emergency stops are within reach‚ and tool‑spindle contacts are guarded․ Regular inspections prevent hazards․ Check tool wear now․
Enclosures‚ Emergency Stops‚ Protective Gear‚ and Machine Lockout
Enclosures on manual CNC machines are designed to contain airborne chips‚ coolant mist‚ and vibration‚ reducing exposure to hazardous particles․ A typical enclosure uses a transparent polycarbonate panel for visibility‚ reinforced steel framing for structural integrity‚ and a vent system that directs airflow away from operators․ The enclosure should be equipped with an interlock that automatically shuts down the spindle when the panel is opened‚ preventing accidental contact with moving parts․ Emergency stops are a critical safety feature; they must be mounted within arm’s reach‚ clearly labeled‚ and wired to cut power to the spindle and drive motors instantly․ A dual‑mode emergency stop—one button for the operator and a secondary one on the control panel—provides redundancy․ Protective gear is mandatory: safety glasses or face shields protect against flying chips‚ gloves shield hands from sharp edges‚ and hearing protection mitigates noise levels that can exceed 90 dB during high‑speed machining․ For prolonged use‚ anti‑fatigue mats reduce operator strain․ Machine lockout procedures involve disconnecting the main power supply‚ applying lockout devices to the main breaker‚ and verifying that all moving components are immobilized before maintenance․ Lockout tags should state the reason and the name of the authorized personnel․ Regular drills and documentation of lockout steps ensure that all operators understand the protocol and can respond quickly in an emergency․ This setup ensures operators can work while producing precise parts for batch runs daily․
Maintenance‚ Calibration‚ and Performance Tuning
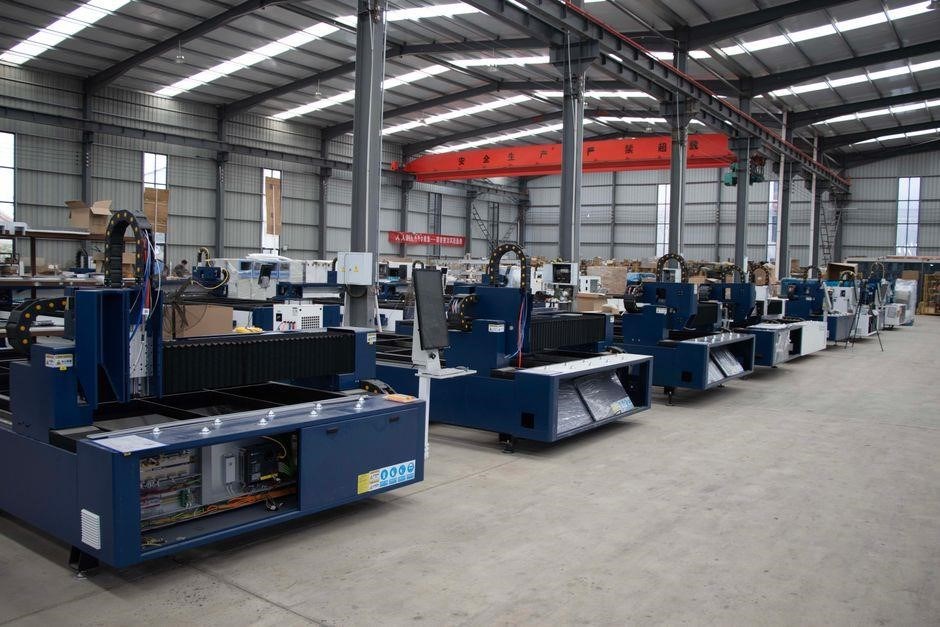
Routine checks‚ alignment‚ zeroing‚ and component replacement keep manual CNC machines accurate and efficient․ Inspect spindles‚ verify linear guides‚ recalibrate axes‚ and replace worn bearings․ Regular lubrication and firmware updates ensure smooth operation and extend machine life and precision for consistent quality
Routine Checks‚ Alignment‚ Zeroing‚ and Component Replacement
Routine inspections keep manual CNCs reliable․ Start by checking spindle bearings for vibration or noise‚ cleaning contact surfaces with isopropyl alcohol‚ and greasing ball‑screws․ Inspect linear rails for debris and runout; any deviation over 0․02 mm warrants adjustment or bearing replacement․ Use a dial indicator to verify X‑‚ Y‑‚ and Z‑axis motion is smooth and free of wobble․
Zeroing is critical before each job․ Engage limit switches or use a calibrated gauge to set the home position‚ record the coordinates in the control software‚ and verify the tool tip aligns with the reference point on the workpiece․ Re‑zero after tool changes or maintenance to maintain accuracy․
Component replacement follows a preventive schedule․ Replace spindle bearings every 500 hours‚ swap worn ball‑screws‚ and upgrade cooling if overheating occurs․ Keep spare linear bearings‚ thrust washers‚ and seals to minimize downtime․
Document every inspection‚ adjustment‚ and part change in a log that includes date‚ operator‚ machine serial‚ and observed anomalies․ This record aids troubleshooting‚ predicts future maintenance‚ and justifies capital upgrades․
Keep a spare set of cutting tools on hand‚ as tool wear can affect surface finish and dimensional accuracy․ Finally‚ schedule a full calibration after any major repair or when the machine has been idle to ensure that all axes remain within tolerance․ All adjustments should be logged daily․ In a secure log․ Regular checks extend machine life․
Applications across Woodworking‚ Metalworking‚ and Hobbyist Projects
Manual CNCs excel in wood panels‚ metal prototypes‚ and hobby builds․ Operators program simple G‑code‚ adjust feeds‚ swap tools for each material‚ achieving detail while keeping costs low․ Ideal for batch production․ now
Custom Parts‚ Prototype Development‚ and Small-scale Production
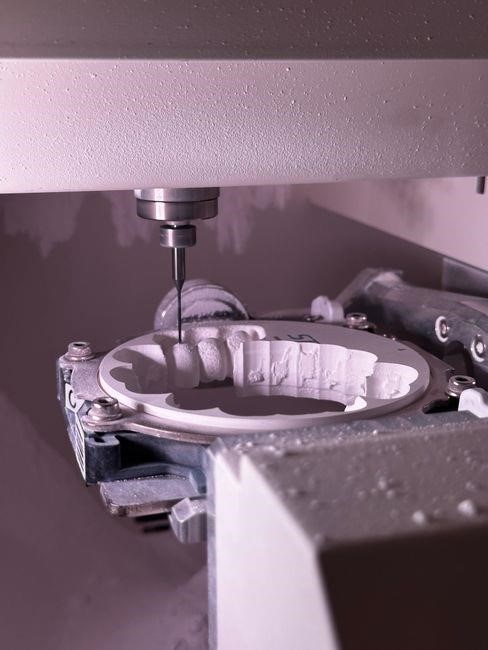
Manual CNC machines empower designers to transform digital concepts into tangible prototypes with remarkable speed and flexibility․ By manually loading G‑code‚ operators can test tool paths‚ tweak feed rates‚ and iterate designs in real time‚ reducing the need for costly re‑machining cycles․ The ability to swap between wood‚ aluminum‚ and composite materials on the same machine enables rapid prototyping across diverse material families․
In small‑scale production‚ manual CNCs serve as the backbone for limited‑run parts‚ such as custom brackets‚ housings‚ or decorative panels․ Operators can adjust cutting parameters for each batch‚ ensuring consistent surface finish and dimensional accuracy while keeping tooling costs low․ The manual interface also facilitates quick tool changes‚ allowing production runs to shift from one part to another without extensive downtime․
Furthermore‚ hobbyists and small workshops benefit from the low entry barrier of manual CNCs․ With basic training‚ users can program complex geometries‚ perform multi‑axis machining‚ and even integrate 3D scanning for reverse engineering․ The combination of hands‑on control and computer precision makes manual CNCs an ideal platform for educational projects‚ product development‚ and artistic expression․
Operators can also perform real‑time adjustments to spindle speed and feed rate‚ allowing quick fine‑tuning of cuts․ The manual interface encourages iterative testing‚ reducing waste and speeding up the fast development cycle․
Future Trends‚ Community Resources‚ and Training Pathways
Emerging trends in manual CNCs focus on hybrid automation‚ AI‑guided toolpaths‚ and modular upgrades․ Communities like Hackaday‚ CNCZone‚ and YouTube tutorials provide free code libraries and training; Workshops and online courses help users master manual operation and advanced programming․ Note
Online Communities‚ Tutorials‚ Emerging Tooling‚ and Software Updates
Manual CNC enthusiasts rely on vibrant forums such as CNCZone‚ Reddit’s r/3Dprinting‚ and the Hackaday community for real‑time problem solving․ Step‑by‑step video tutorials on YouTube and free G‑code repositories empower novices to prototype quickly․ Emerging tooling—compact laser‑guided routers‚ brushless spindle kits‚ and 3‑axis CNC kits—reduces cost and increases precision․ Software updates from open‑source platforms like LinuxCNC and commercial suites such as Mach3 add new safety features‚ advanced interpolation‚ and cloud‑based simulation tools; Regular webinars hosted by tool manufacturers offer hands‑on training‚ while local maker spaces offer workshops that cover spindle calibration‚ tool‑path optimization‚ and safety protocols․
Community-driven resources also include GitHub repositories where users share custom G‑code scripts‚ firmware patches‚ and configuration files for various controllers․ Many makers participate in monthly challenges that push the limits of manual CNCs‚ such as creating intricate lattice structures or complex gear sets with minimal tool changes․ Training pathways range from informal peer-to-peer mentorship in local workshops to structured online courses offered by universities and industry bodies‚ covering topics from basic machine setup to kinematics and safety compliance․ As firmware evolves‚ new features like adaptive tool‑path correction‚ real‑time torque monitoring‚ and cloud connectivity enable operators to fine‑tune performance without leaving the manual control interface